
Essential PLC Skills for Engineering Graduates in Uttarakhand
Contents
Uttarakhand's Industrial Landscape and Automation Demand
Industrial estates across Uttarakhand, such as SIDCUL in Pantnagar, Haridwar, and Rudrapur, host extensive automotive, pharmaceutical, consumer goods, and packaging plants. These facilities rely heavily on automated assembly lines, high-speed packaging machinery, and continuous process control systems. Programmable Logic Controllers (PLCs) form the core execution layer for these automated production lines.
For engineering students and recent graduates in electrical, electronics, instrumentation, or mechanical disciplines, entering these plants requires practical engineering competence rather than pure theoretical knowledge. Understanding what skills are genuinely required on the plant floor helps you prepare effectively before applying for entry-level automation roles.
Electrical Wiring and Hardware Foundations
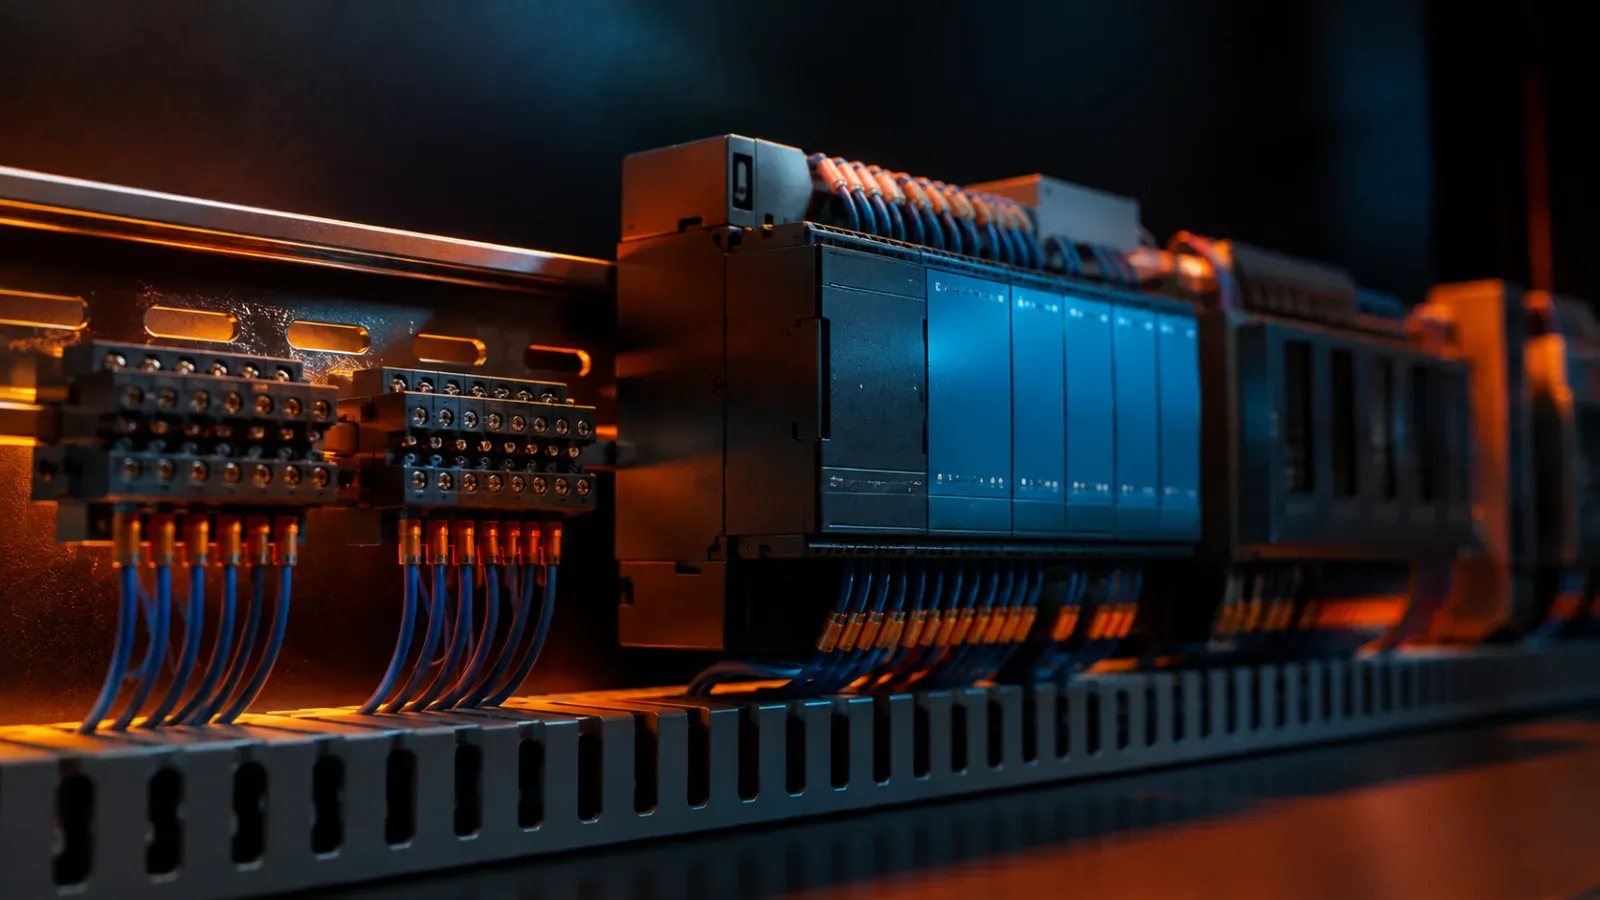
Before writing a single line of PLC code, you must understand control panel wiring and electrical hardware. In an industrial plant, a PLC does not operate in isolation. It interfaces directly with field devices, relay logic circuits, motor starters, and power distribution hardware.
A complete foundation requires mastery of:
- Control Voltage Systems: Understanding 24V DC control loops, 230V AC control power, and isolated industrial power supplies.
- Sinking and Sourcing Logic: Knowing the operational difference between NPN and PNP sensor outputs, and how current flows through PLC digital input and output cards.
- Relays and Contactors: Interfacing PLC transistor or relay outputs to control high-current loads through interposing relays and magnetic contactors.
- Schematic Reading: Interpreting single-line diagrams, terminal strip layouts, and standard electrical control panel schematics.
Without these fundamentals, a programmer cannot diagnose why a digital input LED fails to illuminate or why an output card damaged its circuit due to inductive kickback from an unsuppressed solenoid valve.
Practical PLC Logic and Memory Architecture
Many introductory courses stop at basic ladder logic symbols like Normally Open (NO) and Normally Closed (NC) contacts paired with simple timers and counters. While these are essential building blocks, real plant machinery demands structured programming and deeper memory management.
To build production-ready automation programs, you need to understand:
- Memory Organisation: How PLCs store data across bit memory, integer registers, floating-point words, and structured data blocks.
- Scan Cycle Dynamics: How input image tables update, logic executes sequentially, and output image tables write to physical hardware. Misunderstanding scan execution times can lead to missed high-speed pulses or improper logic timing.
- Analog Signal Processing: Scaling 4-20mA or 0-10V signals from temperature transmitters and pressure transducers using analog-to-digital conversions and linear scaling functions.
- State Machine Design: Structuring operational sequences using sequential function charts or bit-driven state machines rather than unorganised, interlocking ladder rungs.
Fieldbus Networks and HMI Integration
Modern industrial machinery rarely uses hardwired I/O exclusively. Fieldbus communications reduce cable complexity and allow intelligent field devices to transmit diagnostic parameters alongside process values.
A prospective automation engineer should learn:
- Industrial Protocols: Basic operational principles of Modbus RTU/TCP, PROFIBUS, and PROFINET networks, including addressing, baud rates, and cable termination.
- HMI and SCADA Interfacing: Mapping PLC variables to Human-Machine Interface screens, configuring dynamic graphics, alarm banners, and historical trend logs.
- Drive Communication: Sending speed references and run/stop commands to Variable Frequency Drives (VFDs) over serial or Ethernet fieldbuses.
Learning how to establish a stable communication link between a PLC and an HMI or VFD is just as critical as writing the underlying control logic.
Systematic Troubleshooting and Plant Safety
In manufacturing plants across Uttarakhand, unmanaged downtime directly impacts production targets. Employers value engineers who can systematically diagnose hardware and software faults under time pressure while maintaining strict safety standards.
Key diagnostic and safety skills include:
- Online Monitoring: Using PLC programming software to trace active logic, force inputs and outputs safely during commissioning, and read hardware fault buffer logs.
- Multimeter Diagnostics: Testing voltage drops, loop currents, and continuity across terminal blocks to isolate hardware failures from software bugs.
- Industrial Safety Standards: Understanding emergency stop circuits, safety relays, hardware interlocks, and Category 3/4 safety architectures under standard machinery safety guidelines.
Preparing for Your Industrial Automation Career
Acquiring these practical competencies requires hands-on practice with physical hardware, standard programming suites, and realistic industrial scenarios.
NEXISTEK offers technical training courses in industrial automation, PLC programming, SCADA, electrical panel design, and embedded systems. Designed for engineering students and working technical professionals, NEXISTEK's structured curriculum covers hardware wiring, ladder logic, analog processing, and fieldbus networking to help learners build practical engineering skills for modern manufacturing environments.